Blog
10 Tips for Choosing a Non Cartridge Mechanical Seal
Choosing the right Non Cartridge Mechanical Seal can determine whether a pump runs smoothly or stops during a critical shift. The decision involves more than size and price. Shaft diameter, pressure, temperature, fluid characteristics, and installation space all matter. A seal that fits on paper may still fail beside a hot reactor line.
Mechanical-seal specialist Robert J. W. Smith once stated, “A mechanical seal is only as reliable as the conditions surrounding its faces.” That observation remains practical. Clean faces, correct spring compression, and stable lubrication often matter as much as the seal’s material. Small details matter.
This guide presents ten useful tips for selecting a Non Cartridge Mechanical Seal. It considers balanced and unbalanced designs, elastomer compatibility, face combinations, spring materials, and operating limits. It also examines maintenance access, sleeve requirements, and installation accuracy. These points can help engineers compare options before ordering equipment.
Field experience shows that mistakes are rarely dramatic at first. A slightly misaligned shaft may create heat. A dry start can mark the faces within seconds. A poor elastomer choice may swell after several operating cycles. These details are easy to underestimate.
There is no perfect seal for every pump. Sometimes, the lowest purchase price creates the highest maintenance burden. A careful selection still needs verification against drawings, service data, and manufacturer guidance. Even experienced teams can miss one variable. Reflecting on that possibility improves reliability.
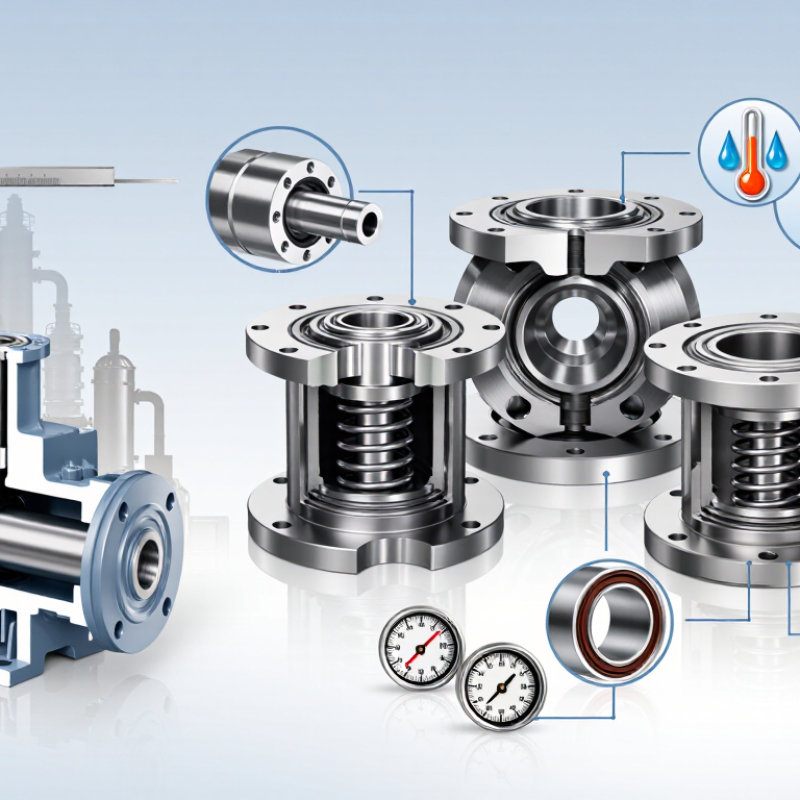
Understanding Non-Cartridge Mechanical Seal Design and Operation
A non-cartridge mechanical seal is assembled directly onto the pump shaft. Its rotating face, stationary seat, springs, and gland require careful field alignment. Unlike cartridge designs, installation depends heavily on shaft measurements and setting dimensions. In practice, a small error can create uneven face loading, heat, and leakage.
Tip 1: Measure shaft runout before fitting the seal.
Tip 2: Confirm the manufacturer’s setting length, not an assumed dimension.
During operation, the seal faces create a thin fluid film. This film reduces friction while maintaining containment. Clean flush fluid matters. Abrasive particles can scratch the faces within minutes. U.S. Department of Energy pumping-system guidance reports that pumping systems may consume 25–50% of industrial motor-system energy. Poor sealing increases losses through friction, leakage, and repeated maintenance.
Tip 3: Check flush pressure, temperature, and cleanliness during commissioning.
Tip 4: Never run the seal dry, even briefly.
Selection should match pressure, speed, temperature, shaft material, and process chemistry. API Standard 682 offers useful design and testing guidance for refinery and process-pump applications. Still, standards do not replace site experience.
Tip 5: Review startup records and previous failure patterns.
Tip 6: Inspect the gland face and sleeve for burrs.
Tip 7: Leave room for adjustment during installation.
A perfectly specified seal can still fail after careless assembly. That uncomfortable detail deserves attention.
Assessing Equipment Requirements and Operating Conditions
Choosing a non-cartridge mechanical seal starts with the equipment, not the seal catalog. Record shaft diameter, chamber depth, mounting length, and shaft endplay before ordering. A few millimeters can matter. Check operating pressure at the seal chamber, rather than relying only on pump discharge pressure. Measure temperature during startup, normal running, cleaning, and shutdown. Speed, vibration, shaft runout, and alignment also affect face stability.
Identify the fluid precisely. Viscosity, abrasives, crystallization, gas content, and chemical compatibility should guide face and elastomer selection. Ask whether the seal may experience dry running during priming or an empty tank. That detail is often missed. Consider the flushing arrangement, available cooling, and surrounding space for installation. A non-cartridge seal needs accurate setting, so confirm the working length with a drawing and a physical measurement.
In field inspections, I have seen suitable seals fail because the chamber was deeper than expected. I have also seen operators choose harder faces for every service, even when heat generation became the real problem. Review pressure, temperature, speed, and material data together. Request documented test conditions when service is critical. Allow for maintenance access and shaft movement. Do not assume the original seal size proves the original selection was correct. Recheck the calculation after real operating data becomes available.
Selecting Suitable Seal Materials and Component Configurations
Tip 1: Start with the pumped fluid, not the seal drawing. Identify temperature, pressure, concentration, viscosity, and abrasive solids. A clean liquid can still crystallize around the seal faces.
Tip 2: Match the face materials carefully. Carbon suits many general services, while silicon carbide handles abrasion and difficult fluids better. Tungsten carbide can tolerate impact, but it may not fit every chemical environment. Tip 3: Check chemical compatibility for elastomers. EPDM, FKM, and PTFE each respond differently to heat, oils, solvents, and additives. Never rely on a familiar material without reviewing real operating data. Tip 4: Choose balanced or unbalanced construction according to pressure. Balanced designs usually reduce face loading at higher pressures. This detail is easy to overlook.
Tip 5: Select pusher, non-pusher, or bellows configurations based on movement and contamination risks. Pusher seals may tolerate some axial movement, but sliding parts can collect deposits. Tip 6: Confirm whether a single or double seal is necessary. A double arrangement can support hazardous or highly volatile fluids when the support system is correctly designed.
Tip 7: Inspect shaft size, sleeve condition, runout, and surface finish before ordering components. A well-made seal cannot correct a damaged shaft. Tip 8: Review spring placement and rotation direction. Internal springs may clog in dirty service. Tip 9: Verify flushing, quenching, and cooling connections with the actual equipment layout. Tip 10: Request material certificates and test records when reliability matters. In practice, my first material choice is sometimes wrong. Small pilot tests and operating feedback should change the final configuration.
Checking Installation Space, Alignment, and Maintenance Needs
When choosing a non-cartridge mechanical seal, inspect the installation space before comparing seal materials. Measure shaft diameter, stuffing-box depth, face dimensions, and gland-bolt spacing. Check the available room for tools, hands, and future seal removal. Access matters. A seal that fits on paper may become difficult to service beside a pipe or guard. Leave enough clearance for a dial indicator and controlled tightening.
Alignment deserves equal attention. Measure shaft runout near the seal location, then check coupling alignment and bearing condition. Excessive movement can overload the seal faces, even when the nominal dimensions are correct. A soft foot or bent shaft may look like a seal failure. I have seen maintenance teams replace seals repeatedly before checking these basic conditions. That mistake is expensive, but easy to repeat. Record measured values instead of relying on memory or old drawings.
Maintenance needs should influence the seal design and installation method. Confirm whether technicians can inspect faces, replace elastomers, and clean the chamber without removing major equipment. Review the process temperature, pressure, solids, and flushing requirements with qualified personnel. Keep spare parts protected from heat, dust, and sunlight. Use a torque wrench and follow a documented tightening sequence. Small errors matter. One practical improvement is photographing the original assembly before removal. My own field notes are not always complete, so a second inspection is worthwhile. A short trial run with monitored leakage can reveal installation problems before they become serious.
10 Tips for Choosing a Non Cartridge Mechanical Seal - Checking Installation Space, Alignment, and Maintenance Needs
| Tip | Selection Dimension | What to Check | Practical Guidance | Why It Matters |
|---|---|---|---|---|
| 1 | Shaft or Sleeve Diameter | Measure the actual shaft or sleeve diameter at the seal location and compare it with the seal size range. | Use calibrated measuring tools. Confirm the shaft is round, free from burrs, and within the equipment manufacturer’s dimensional tolerance. | An incorrect diameter can prevent proper clamping, cause leakage, or create excessive face loading. |
| 2 | Available Installation Space | Check axial length, radial clearance, gland access, bolt clearance, and room for tools. | Compare the available seal chamber dimensions with the seal drawing before ordering. Allow enough space to tighten fasteners evenly. | Non-cartridge seals are assembled in place; limited access can make installation inaccurate and maintenance difficult. |
| 3 | Shaft Runout | Measure radial shaft movement near the seal faces with a dial indicator while rotating the shaft by hand. | Use the pump or equipment specification as the controlling limit. Excessive runout should be corrected before selecting or installing the seal. | Runout can flex the seal faces, producing uneven wear, heat generation, and leakage. |
| 4 | Shaft and Equipment Alignment | Verify coupling alignment, bearing condition, shaft concentricity, and equipment mounting. | Correct soft foot, worn bearings, pipe strain, or coupling misalignment before commissioning. | A seal cannot compensate for poor equipment alignment or unstable shaft movement. |
| 5 | Operating Pressure and Speed | Confirm pressure, temperature, shaft speed, pressure fluctuations, and start-up conditions. | Select a seal whose documented operating limits cover normal, maximum, and transient conditions. | Pressure and speed affect face loading, heat generation, spring performance, and seal life. |
| 6 | Fluid Compatibility | Identify the process fluid, concentration, suspended solids, crystallization tendency, and chemical additives. | Check compatibility of the faces, secondary elastomer, spring, metal parts, and gasket materials with the complete fluid composition. | Chemical attack, swelling, abrasion, or clogging can cause premature leakage. |
| 7 | Seal Face Material | Consider lubrication, abrasives, dry-running risk, temperature, and chemical exposure. | Use hard, wear-resistant face combinations for abrasive service and suitable low-friction combinations for clean, lubricating fluids. | The face pairing controls wear rate, frictional heat, and resistance to fluid-related damage. |
| 8 | Setting and Installation Method | Determine how the seal spring compression or working length will be established during installation. | Use the specified setting dimension, installation instructions, and clean assembly practices. Do not guess the spring setting. | Incorrect setting can result in insufficient contact pressure or excessive friction and wear. |
| 9 | Maintenance Access and Spare Parts | Review the time required to remove the gland, springs, faces, gaskets, and other replaceable components. | Choose a design with accessible components, clear replacement instructions, and readily available standard spare parts. | Good maintainability reduces downtime and lowers the risk of installation errors during repairs. |
| 10 | Monitoring and Flushing Requirements | Check whether the application needs clean flush fluid, cooling, quenching, pressure monitoring, or leakage detection. | Provide the required auxiliary connections and verify that flush flow, pressure, and temperature can be monitored. | Proper environmental control removes heat and solids, improves face lubrication, and extends service life. |
Comparing Performance, Reliability, Cost, and Supplier Support
Choosing a non-cartridge mechanical seal requires more than comparing purchase prices. Performance depends on face materials, spring design, shaft condition, flush planning, and installer skill.
In a refinery pump room, seals may face heat, abrasive solids, pressure cycling, or dry starts. ISO 21049, also known as API 682, offers selection guidance, but site-specific judgment remains essential. A seal suited to clean water may fail quickly in slurry. Small details matter.
Cost deserves a lifecycle view. The U.S. Department of Energy’s Improving Pumping System Performance sourcebook estimates that pumping systems consume about 27% of industrial electricity in the United States. Its Operations and Maintenance Best Practices guide also reports potential savings of 5–20% through effective maintenance.
A low-cost seal can become expensive when technicians need repeated alignment checks. Non-cartridge designs often demand careful measurement and assembly. Those labor hours are easily omitted from quotations. I have seen budgets ignore downtime. That mistake is costly.
Reliability should be judged through evidence, not confident language. Request test conditions, failure records, material certificates, installation tolerances, and response-time commitments.
The Hydraulic Institute’s Pump System Assessment Tool reinforces a practical point: seal reliability depends on pump operation, not only seal geometry. Supplier support is part of performance.
Specify troubleshooting access, site attendance, root-cause reports, training, and stocked components. For critical equipment, compare one lost production shift against annual seal savings.
The cheapest option may win on paper. Sometimes, paper is wrong.

